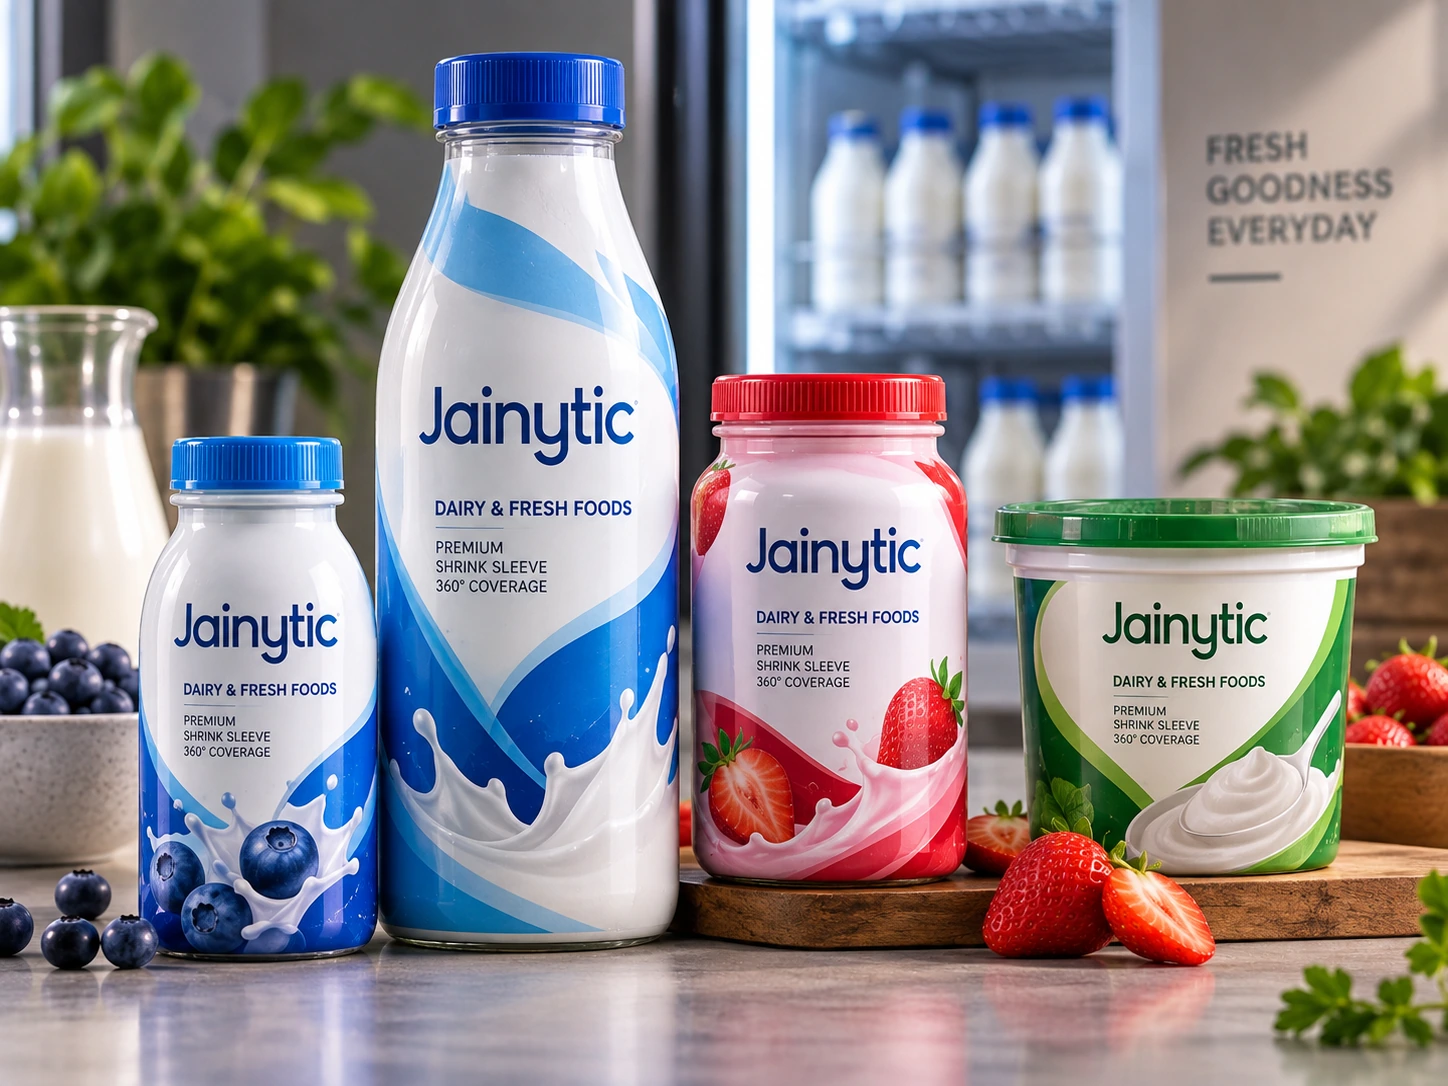
A Premium Sleeve for a Contoured Bottle
A packaging converter received an order for printing PET-G shrink sleeves for a premium dairy beverage brand. The customer required:
- High gloss appearance
- Reverse printed graphics
- High shrink performance without ink cracking
The sleeves were intended for contoured PET bottles with full-body decoration.
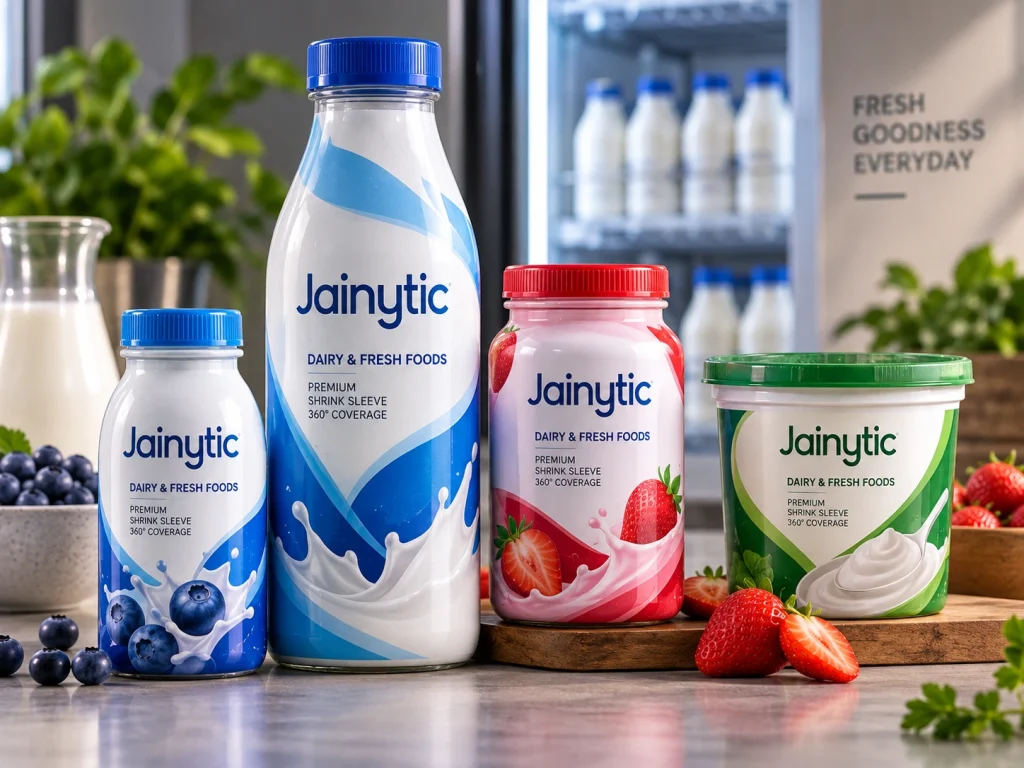
What the Job Demanded
- Film Type
PET-G Shrink Film
- Printing Process
Flexographic Printing
- Colours
10 Colours
- Printing Side
Reverse Printing
- Shrink Tunnel
Steam Tunnel
- Sleeve Type
Full Body Sleeve + Neck Seal
Three Problems, Solved at the Root
Three issues surfaced during production. Each was traced to its root cause and corrected.
Ink Cracking After Shrink
After steam shrinking:
- White ink and dark solid areas developed cracks
- Graphics became visually damaged
Root cause
Ink flexibility was insufficient for high TD shrinkage of PET-G film.
Solution provided
- Changed to high-flexibility shrink sleeve ink system
- Reduced ink film thickness
- Modified drying temperature
Result
Cracking reduced significantly during shrink application.
Curling of Printed Film
Printed reels showed edge curling after rewinding.
Root cause
- Excess drying temperature
- Uneven tension profile
- Solvent retention imbalance
Solution provided
- Reduced dryer temperature from 65°C to 55°C
- Balanced air flow
- Optimized rewind tension
Result
Flat reel formation achieved.
Sleeve Seam Failure
Some sleeves opened during steam shrinking.
Root cause
- Ink contamination at seam area
- Poor adhesive anchorage
Solution provided
- Reduced print overlap near seam
- Improved seam adhesive compatibility
- Increased seam curing time
Result
Seam strength improved and tunnel rejection reduced.
The Outcome on the Production Line
Print QualityExcellent
Shrink AppearanceSmooth
Production Efficiency94%
Customer ComplaintsReduced by 85%
Machine Speed StabilityImproved
What This Job Taught Us
- 01PET-G requires highly flexible shrink sleeve inks.
- 02Tension control is critical in flexo printing.
- 03Excess drying temperature can deform shrink films.
- 04Seam area must remain clean for proper bonding.
- 05Reverse printing requires careful solvent management.
- 06Anilox selection directly affects shrink performance.
The Work, Up Close